 Jiuju Automation
Stator-Rotor Press-Fit Drift on Drone Pancake Motors? Jiuju's Integrated Magnet Insertion Equipment
138无人机盘式电机节拍优化先做时间分析,久巨用并行化、动作合并与快换在不越质量红线的前提下提速。
View Full Version磁钢混线生产换型时间长是插磁车间痛点,模块化夹具与参数记忆可大幅压缩。
It’s not about changing the fixture itself, but rather finding the right program, adjusting parameters, and running test runs. We analyzed the data from a client’s magnetic insert workshop in Dongguan and found that the average downtime for changeovers was 47 minutes, of which fixture replacement accounted for only 8 minutes; the remaining 39 minutes were spent adjusting insertion depth, positioning speed, and the orientation of the magnetic inserts. The reason for this was that the program names stored on each machine were disorganized, and operators entered them based on experience.

Step 1: Design the fixture with a quick-change mechanism using pneumatic locking or positioning pins, with the goal of reducing fixture changeover time to less than 3 minutes; Step 2: Create a product recipe library in the PLC, saving settings for magnet length, insertion depth, and insertion speed under model-specific names so they can be automatically loaded upon retrieval; Step 3: Set up mandatory first-piece verification; automatic operation is only enabled after 10 consecutive pieces pass inspection. After implementing SMED, this client’s changeover time was reduced from 47 minutes to 15 minutes.
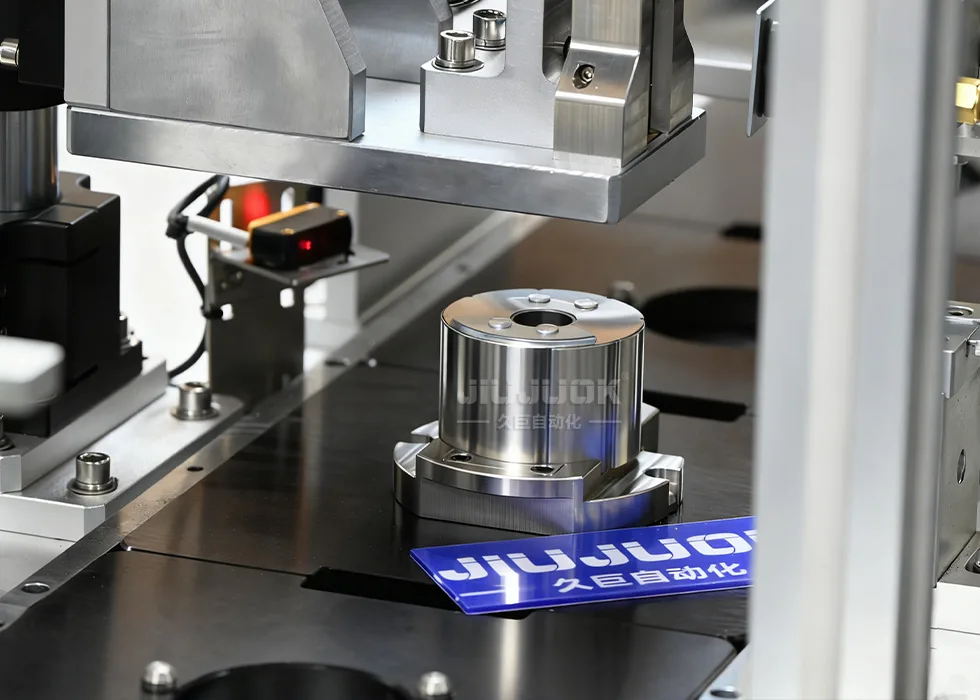
在料仓入口加视觉识别,比对磁钢尺寸和当前配方是否一致;插装工位前增加光电检测,确认磁钢极向。我们曾经遇到一批N42和N48混料的情况,视觉分选后拦截了12片错料。另外建议把相似型号错开排产,颜色或高度差异小的磁钢不要连续换型,给操作工留出核对时间。

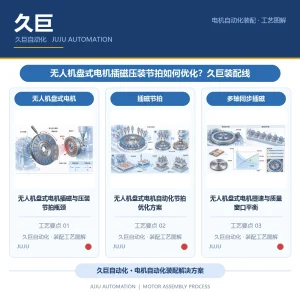
无人机盘式电机节拍优化先做时间分析,久巨用并行化、动作合并与快换在不越质量红线的前提下提速。
View Full Version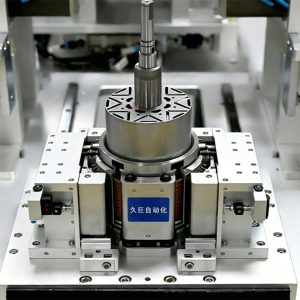
In response to the needs of the low-altitude economy and the power requirements of drones, Jiuju Automation has launched an automated production line for drone motors, improving thrust-to-weight ratio and consistency, and helping drone OEMs reduce costs through mass production.
View Full Version
Jiuju Automation has designed a magnet insertion machine for the assembly of integrated permanent magnet (IPM) rotors and surface-mount magnets, ensuring precise pole spacing and high production efficiency.
View Full Version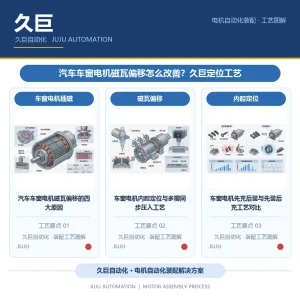
车窗电机的磁瓦偏移是最隐蔽的缺陷之一:偏移量不大时电机照样能转,只是噪音偏高、升降变慢、电流上升,等到整车厂反馈玻璃升降发卡,问题已经批量流出。
View Full Version 简体中文 简体中文
 English
 Español
 Français
 Deutsch (Sie)
 العربية
 Русский
 हिन्दी
 한국어
 ไทย
 Tiếng Việt